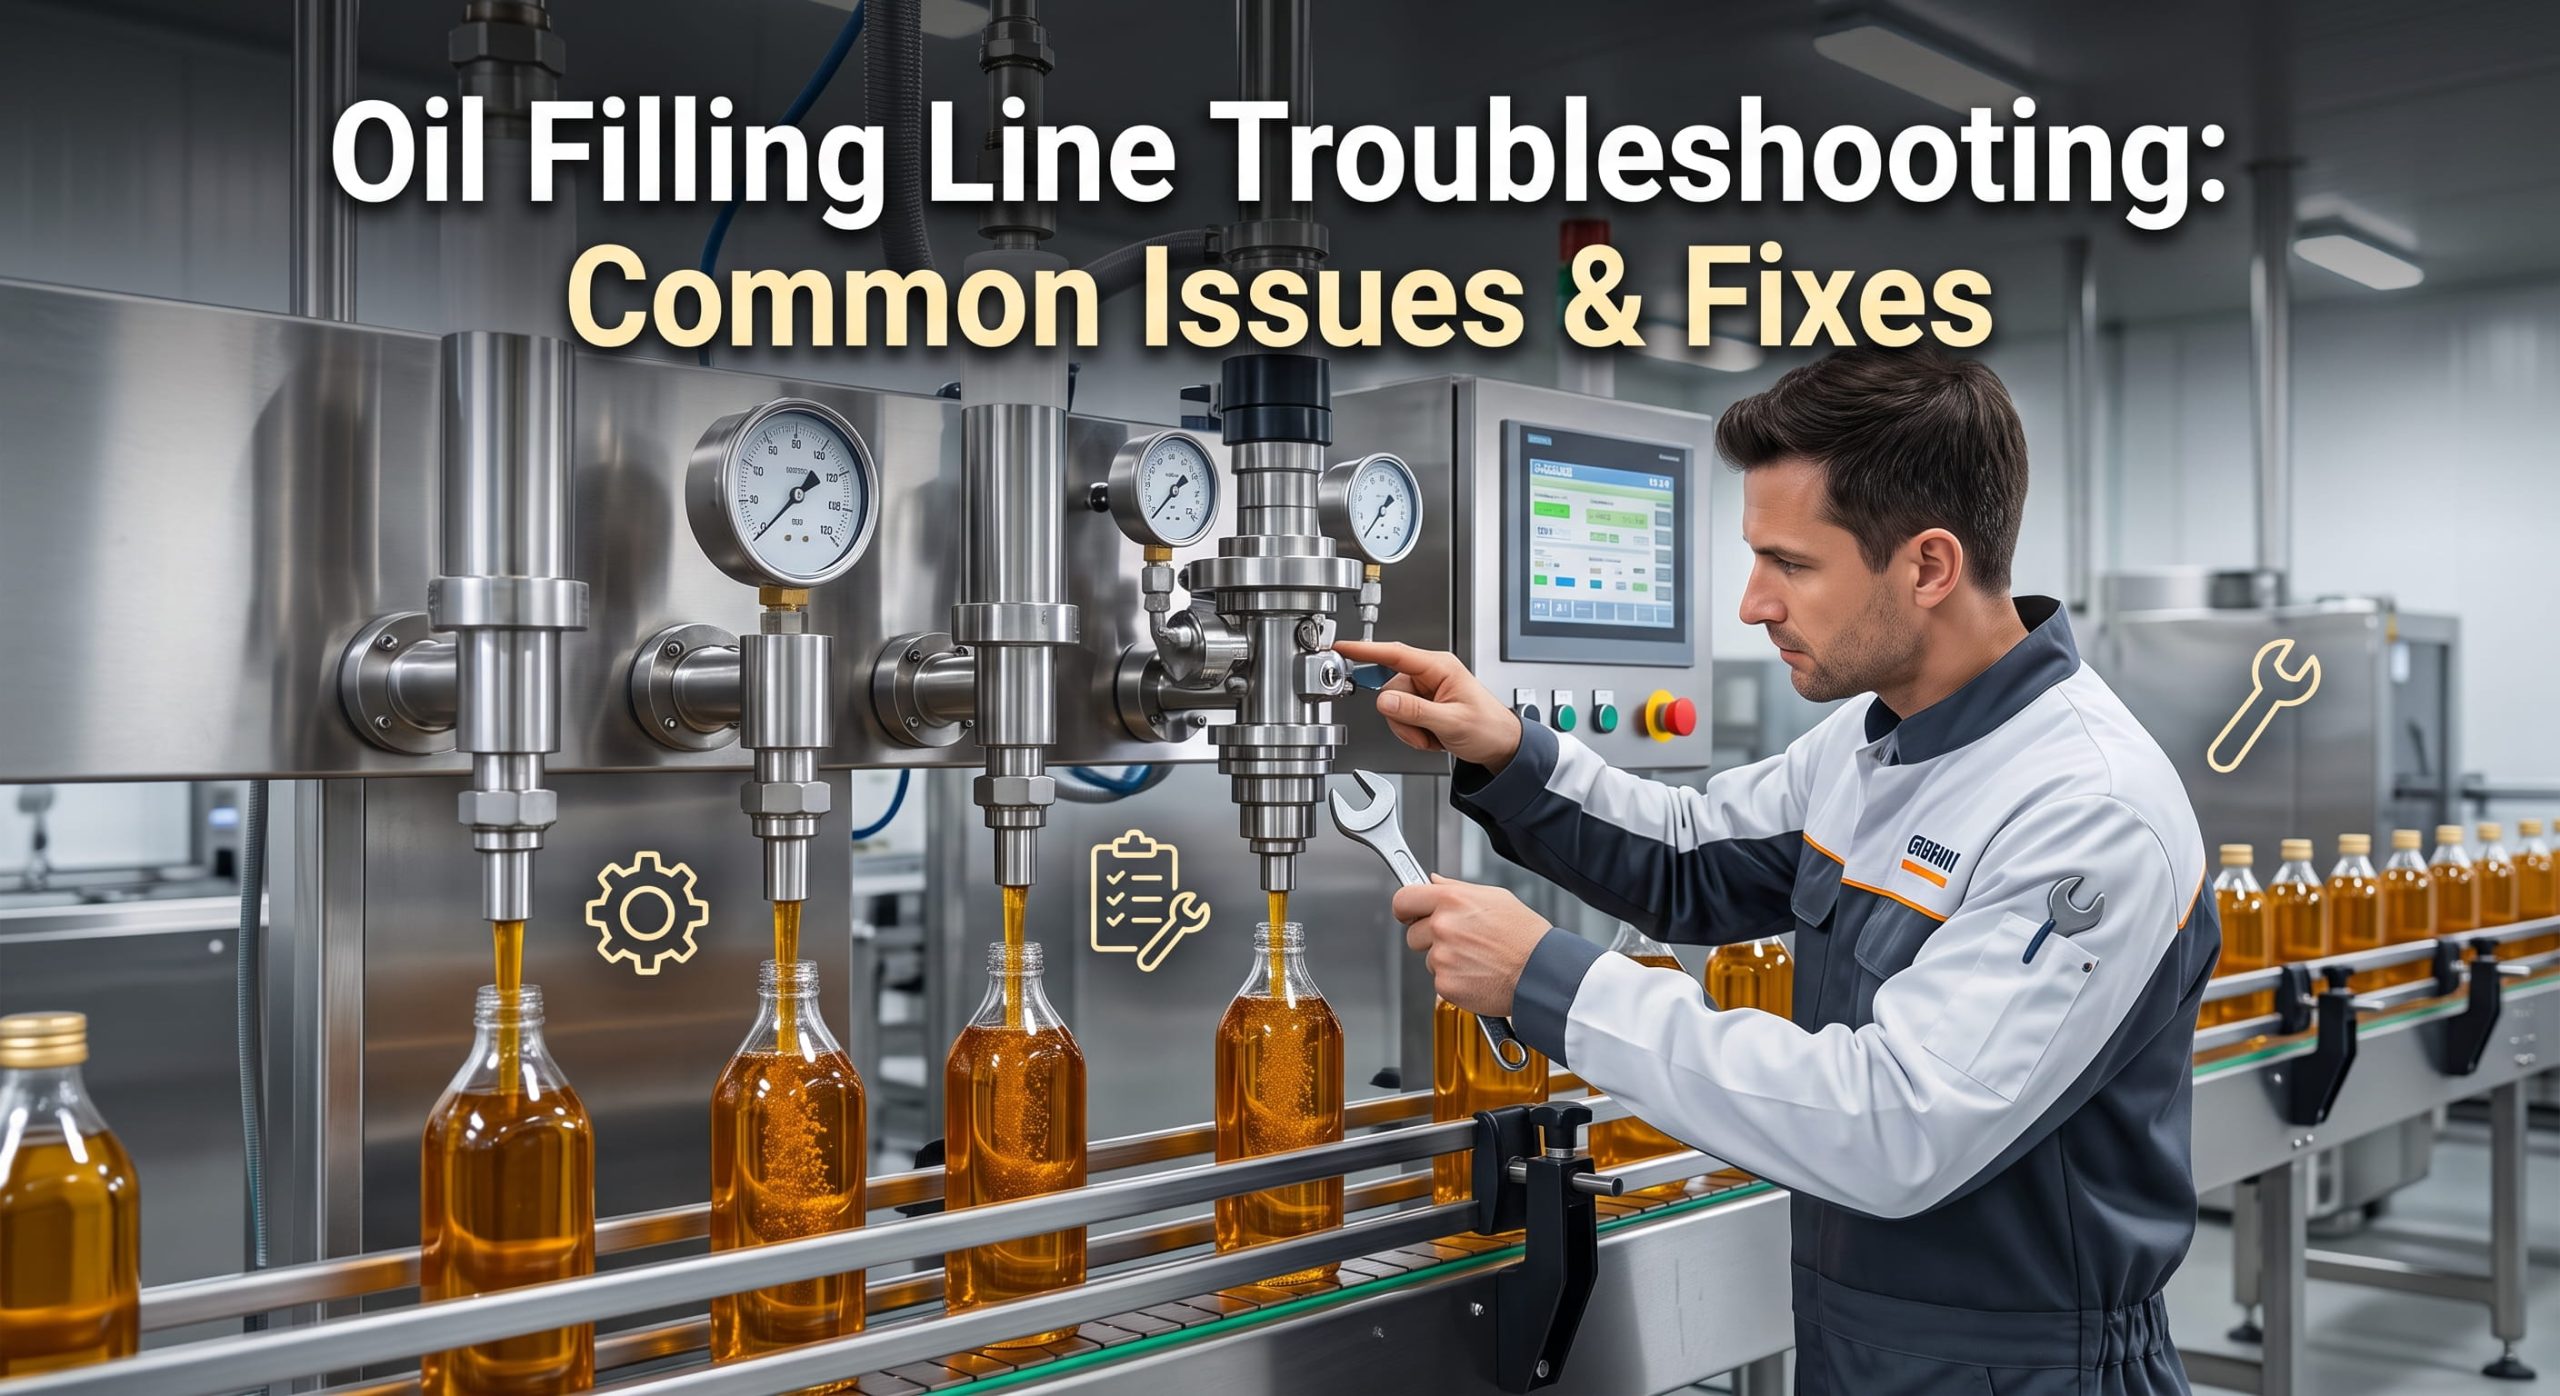
Oil filling lines face different challenges than water or thin-liquid lines. Viscosity changes with temperature, product residue builds up, and pumps wear faster. These issues cause inconsistent fills, leaks, and unexpected downtime.
This article covers the ten most common problems in edible oil and high-viscosity liquid filling. For each problem, you will find the root causes, step-by-step fixes, and preventive measures. The goal is simple: help you reduce downtime and protect product quality.
Quick Reference: Troubleshooting by Oil Behavior
Use the quick reference table below to match common oil behaviors to likely causes and recommended adjustments.
| Oil Behavior | Likely Issue | Recommended Adjustment |
|---|---|---|
| Thin oil splashing | Overflow | Reduce speed; lower nozzle |
| High-viscosity oil | Incomplete fill | Increase pressure; adjust piston |
| Oil with bubbles | Aeration | Slow fill; bottom-up filling |
| Stringy oil | Nozzle dripping | Anti-drip nozzle; suck-back control |
| Temperature-sensitive oil | Changing fill volume | Stabilize oil temperature |
| Oil residue buildup | Contamination | Increase cleaning frequency |
Now let us examine each problem in detail.
1. Inconsistent Fill Levels in Edible Oil Filling
Temperature shifts, air bubbles, and mechanical wear are the primary causes of inconsistent fill levels in oil filling lines.
Why Fill Volume Drifts in Oil Filling
Several factors cause fill volume to change over time:
- Viscosity changes with temperature. A 10°C rise can increase flow rate by up to 15% in some oils.
- Air bubbles disrupt dosing, especially in high-viscosity products.
- Pump wear introduces gradual deviation.
- Calibration drift occurs over time, especially in lines running multiple oil types.
Troubleshooting Steps
- Check fill parameters and verify product temperature.
- Inspect valves and seals for wear.
- Calibrate the machine using a flow meter or volumetric check.
- Record proven settings for each oil type and viscosity range.
Prevention
- Schedule routine calibration at fixed intervals.
- Monitor oil temperature and adjust fill settings accordingly.
- Use servo-driven filling for automatic compensation of viscosity changes. Our servo systems achieve fill accuracy of ±0.2% to ±0.5%.
2. Nozzle Dripping and Post-Fill Leakage
Degraded O-rings, delayed valve closure, and vacuum backflow are the most common causes of nozzle dripping in oil filling lines.
Root Causes for Oil Filling
- O-ring degradation from repeated heating and cooling cycles.
- Valve timing lag, especially in pneumatic systems.
- Vacuum backflow when filling high-viscosity oil.
- Nozzle misalignment after changeover.
Troubleshooting Steps
- Inspect nozzle seals and replace if brittle or worn.
- Check shutoff valve timing and adjust if needed.
- Clean nozzles to remove oil residue.
- Verify nozzle alignment during setup.
Prevention
- Establish a nozzle cleaning routine after each shift.
- Monitor seal wear and replace at scheduled intervals.
- Use anti-drip nozzles with suck-back control for high-viscosity oils.
3. Air Bubbles and Foaming in Oil Filling
High filling speed, excessive nozzle height, and turbulence during transfer are the main causes of air bubbles and foaming in oil filling.
Causes Specific to Edible Oil
- High-viscosity oil traps air more easily during fast filling.
- Temperature changes affect oil surface tension and foam formation.
- Pump cavitation introduces air into the product.
- Transfer systems with sharp bends create turbulence.
Troubleshooting Steps
- Reduce fill speed and use two-stage filling.
- Lower nozzle position to fill from the bottom up.
- Adjust pump settings to minimize turbulence.
- Use specialized nozzles or anti-foam equipment if needed.
Prevention
- Test filling behavior for each new oil product.
- Use product-specific settings stored in the HMI.
- Keep oil temperature stable throughout the shift.
4. Slow Production Speed in Oil Filling Lines
Mechanical wear, poorly optimized settings, and clogged components are the primary causes of slow production speed in oil filling lines.
Causes in Edible Oil Applications
- High-viscosity oil flows more slowly through lines and valves.
- Clogged filters and nozzles reduce flow rate.
- Worn pumps lose efficiency over time.
- Outdated control systems cannot adjust speed for viscosity changes.
Troubleshooting Steps
- Follow a strict preventive maintenance schedule.
- Clean lines and nozzles thoroughly to remove oil residue.
- Optimize electrical systems and confirm parameters match product specs.
- Consider servo-driven filling for programmable speed control.
Prevention
- Schedule regular cleaning and maintenance.
- Monitor pump performance and replace worn components.
- Use viscosity-based speed controls.
5. Hygiene and Contamination in Oil Filling
Poor cleaning practices, oil residue buildup, and unhygienic equipment design are the main causes of contamination in oil filling lines.
Causes in Edible Oil Production
- Oil residue builds up in pipes, valves, and nozzles.
- CIP systems may not fully remove high-viscosity oil without proper cleaning agents.
- Equipment with crevices or dead corners traps oil.
- Neglected maintenance schedules increase contamination risk.
Troubleshooting Steps
- Establish strict cleaning protocols for oil-based products.
- Use stainless steel or hygienic materials that are easy to clean.
- Incorporate sanitation checks into daily operations.
- Schedule deep cleans between product changeovers.
Prevention
- Use CIP-compatible equipment with sanitary design.
- Train operators on oil-specific cleaning procedures.
- Monitor cleaning effectiveness with visual checks.
6. Pump and Pressure Mishaps in Oil Filling
Worn components, incorrect pressure settings, and clogs in lines are the primary causes of pump and pressure problems in oil filling.
Causes in High-Viscosity Applications
- High-viscosity oil increases internal friction and pump wear.
- Particulate buildup from oil residue clogs lines.
- Incorrect pressure settings cause overpumping or underfilling.
- Lack of regular service leads to sudden breakdowns.
Troubleshooting Steps
- Inspect pumps frequently for wear.
- Replace damaged components before they fail.
- Adjust pressure systems to match oil viscosity.
- Clear obstructions in lines immediately.
Prevention
- Schedule monthly seal inspections.
- Use hardened-steel pump components for viscous oils.
- For oils above 300 cSt, use progressive cavity or gear pumps instead of centrifugal designs.
7. Container Misalignment and Jams in Oil Filling
Misaligned conveyors, defective guide rails, and worn moving parts are the primary causes of container misalignment and jams in oil filling lines.
Causes in Edible Oil Lines
- Oil residue on conveyor tracks affects container movement.
- Worn guide rails allow bottles to shift.
- Improper container placement by operators.
- Inconsistent bottle shapes from different suppliers.
Troubleshooting Steps
- Realign conveyor systems and replace worn guide rails.
- Train operators on proper container loading.
- Incorporate alignment checks into routine inspections.
- Clean conveyor tracks regularly to remove oil buildup.
Prevention
- Use proper format parts for each bottle type.
- Verify alignment during every changeover.
- Schedule routine conveyor maintenance.
8. Capping and Sealing Issues in Oil Filling
Misaligned caps, defective capping heads, and torque calibration errors are the primary causes of capping and sealing issues in oil filling lines.
Causes in Edible Oil Packaging
- Oil residue on cap threads prevents proper sealing.
- Torque settings drift over time.
- Inconsistent cap quality from suppliers.
- Capping heads wear faster with oily products.
Troubleshooting Steps
- Recalibrate torque settings regularly.
- Inspect capping heads for wear or damage.
- Verify cap and container compatibility.
- Clean cap chutes and capping heads to remove oil film.
Prevention
- Proactive inspections before each shift.
- Use caps designed for oil-based products.
- Schedule regular torque calibration.
9. Overheating and Electrical Failures in Oil Filling
Faulty wiring, poor ventilation, and overloaded circuits are the primary causes of overheating and electrical failures in oil filling lines.
Causes in Edible Oil Production
- Oil residue on motors and electrical components traps heat.
- Poor ventilation in production areas.
- Aging electrical components fail under continuous load.
- Insufficient cooling systems for high-speed lines.
Troubleshooting Steps
- Improve ventilation around motors and control panels.
- Inspect wiring regularly for wear or loose connections.
- Replace outdated components.
- Avoid overloading circuits.
Prevention
- Schedule electrical audits.
- Keep motors and electrical components clean and free of oil.
- Use frequency-controlled motors to reduce heat and energy use.
10. Sensor and Detection Errors in Oil Filling
Dirty sensors, misalignment, and internal defects are the primary causes of sensor and detection errors in oil filling lines.
Causes in Edible Oil Applications
- Oil film on sensors interferes with readings.
- Dust and humidity impair sensor accuracy.
- Sensors not recalibrated routinely.
- Vibration from pumps affects sensor alignment.
Troubleshooting Steps
- Clean sensors regularly to remove oil residue.
- Recalibrate sensors as part of routine maintenance.
- Replace defective sensors promptly.
- Check sensor alignment after pump maintenance.
Prevention
- Use oil-resistant sensor housings.
- Schedule monthly sensor calibration.
- Keep spare sensors in stock.
Preventive Maintenance Checklist for Oil Filling Lines
A consistent maintenance schedule prevents most of the problems covered above. The following checklist is based on common industry practice:
- Monthly sensor calibration
- 500-hour pump inspection
- 400-hour piston seal replacement
- Per-batch viscosity monitoring
- Scheduled nozzle and valve cleaning
- Daily or weekly inspections for leaks, residue, cracks
- Performance monitoring: fill volumes, cycle times, output
- Quality control checks on filled containers
- Keep critical spare parts on hand: seals, nozzles, gaskets, sensors
How to Identify Oil Filling Problems Early
Early detection is the difference between a quick adjustment and a costly shutdown. The following practices help operators catch small issues before they escalate.
Conduct Regular Inspections
Daily or weekly walkthroughs are the simplest defense against unexpected failures. Look for leaks, oil residue, or cracks. Use a structured checklist to maintain consistency.
Monitor Performance Consistently
Record fill volumes, cycle times, and output levels. A gradual decline in fill accuracy may indicate calibration drift. Sudden drops in speed could mean component wear.
Perform Quality Control Checks
Sample filled containers for volume, sealing, and labeling. Small irregularities may point to underlying equipment problems.
Leverage Data and Sensors
Smart sensors and digital monitoring provide real-time feedback on temperature, pressure, and performance. Set alerts for anomalies to allow rapid response.
How Servo-Driven Filling Reduces These Problems
Servo-driven filling addresses several common oil filling issues. Our servo systems provide:
- Fill accuracy of ±0.2% to ±0.5%, compared to ±1.0% for traditional piston fillers.
- Programmable speed control for different oil viscosities.
- Recipe storage for fast changeover between oil types.
- Fewer mechanical parts, reducing wear and maintenance.
- Real-time data for traceability and predictive maintenance.
For manufacturers running multiple oil types or facing frequent viscosity changes, servo-driven filling reduces the root causes of many problems covered in this article.
When to Contact an Expert
Some issues go beyond what on-site staff can resolve. Consider contacting an expert in the following situations:
- Problems persist after thorough troubleshooting.
- Electrical or software malfunctions are suspected.
- Production downtime is critical and extended delays are unacceptable.
- Specialized upgrades or custom parts are required.
- Safety concerns exceed in-house expertise.
- Machine is due for a comprehensive performance audit.
Conclusion
Most oil filling line issues can be prevented or resolved with routine maintenance, proper calibration, and operator training. Early detection and knowing when to call an expert reduce downtime and protect product quality.
If you need help diagnosing a persistent problem or selecting the right filling equipment for edible oil and high-viscosity liquids, contact Modern Machinery. Our team can help you choose the right servo-driven filling solution for your production goals.
Contact Modern Machinery today to discuss your production requirements and request a free layout and quote.
Frequently Asked Questions
Why does my oil filling machine show inconsistent fill levels?
Temperature shifts, air bubbles, mechanical wear, and inadequate calibration are common causes. Check oil temperature, inspect seals, and recalibrate.
What causes nozzle leakage after filling oil?
Degraded O-rings, delayed valve closures, vacuum backflow, and nozzle misalignment. Replace seals and check valve timing.
How can electrical failures affect oil filling operations?
They cause intermittent stops, startup delays, control panel malfunctions, and overheating. Inspect wiring and improve ventilation.
What preventive maintenance is recommended for oil filling machines?
Monthly sensor calibration, 500-hour pump inspections, 400-hour piston seal replacement, per-batch viscosity monitoring, and regular cleaning.
When should I replace sensors on my oil filling machine?
If they consistently misread despite cleaning and recalibration, they may be defective. Replace promptly.
What preventive steps can I take to avoid downtime?
Follow a strict maintenance schedule, train staff, keep spare parts, and conduct regular inspections and quality checks.
Can servo-driven filling handle high-viscosity oils?
Yes. Servo systems are ideal for edible oil, sauce, syrup, and other viscous products. The programmable speed control prevents splashing and ensures accurate fills.